PPAP (Production Part Approval Process)
PPAP (Production Part Approval Process) is a standardized procedure for the formal approval of products and processes in industrial series production. Its aim is to provide documented evidence that a supplier can manufacture a product under series production conditions in line with all technical, legal and customer-specific requirements.
PPAP is a central element of quality management in the automotive industry and is closely linked to the requirements of IATF 16949. It connects product development, process planning and series production in a formal approval process.
The Role of PPAP in Product Development
PPAP is typically part of structured product development processes such as APQP. While APQP defines the planning and validation phases, PPAP provides formal evidence that the planning results have been implemented successfully.
PPAP fulfills the following functions:
- verifying the conformity of product and process,
- documented customer approval before the start of series production,
- ensuring reproducibility under series production conditions,
- transparent evidence as part of quality assurance.
Elements of a PPAP Submission
A complete PPAP submission consists of a defined number of standardized records. The exact scope depends on the agreed submission level. Typical elements are:
- design drawings and specifications,
- change documentation,
- design and process FMEA (FMEA),
- process flow diagram,
- control plan,
- evidence of measurement and inspection equipment capability,
- material records,
- initial sample inspection report (ISIR),
- evidence of process capability,
- Part Submission Warrant (PSW) as the formal approval declaration.
Together, these documents demonstrate the supplier’s ability to manufacture a product consistently and in line with specifications.
Submission Levels
PPAP defines different submission levels that determine the scope of the documentation to be submitted. They range from submitting only the PSW to submitting all records in full.
The level is agreed between customer and supplier and is based on the risk classification, product complexity and scope of changes.
Relationship to Process Capability
A central element of PPAP is evidence of process capability. Statistical indicators are used to demonstrate that the process operates stably within defined tolerances. Methods of statistical process control support this evaluation.
The initial process capability study serves as the basis for series release and as the reference for later ongoing process monitoring.
PPAP vs. Initial Samples and Series Inspection
PPAP is not the same as a single initial sample or an isolated inspection report. It is a comprehensive approval procedure that combines product, process and documentation evidence.
Series inspections and ongoing quality monitoring take place after PPAP approval and are part of continuous process control.
PPAP in the Context of Standards
PPAP is an industry-specific procedure of the automotive industry and part of the requirements of IATF 16949. IATF 16949 is based on the principles of ISO 9001 and extends them with specific requirements for product and process approval.
PPAP is therefore an operational tool within a quality management system based on standards.
FAQ
What does PPAP stand for?
PPAP stands for Production Part Approval Process and refers to a standardized procedure for the formal approval of products and processes before the start of series production.
When is a PPAP carried out?
A PPAP is carried out for new parts, product changes, process changes, relocations of production or at the customer’s request.
Is PPAP only relevant to the automotive industry?
PPAP is primarily established in the automotive industry, but it can also be applied in other industries with comparable approval requirements.
What role does process capability play in PPAP?
Process capability is a central part of PPAP evidence and demonstrates that the production process operates stably and in line with specifications under series production conditions.
Standards and Norms
- IATF 16949 – Quality management in the automotive industry
- ISO 9001 – Quality management systems
- Quality management
- Quality assurance
- Statistical process control
- Production Part Approval Process
Further Internal Content
- APQP as the overarching product development process
- The control plan as part of the PPAP submission
- Initial sampling and PPAP in the CAQ system
AI-assisted · Editing and publication: Christian Sedlag · Last updated: 9 November 2026
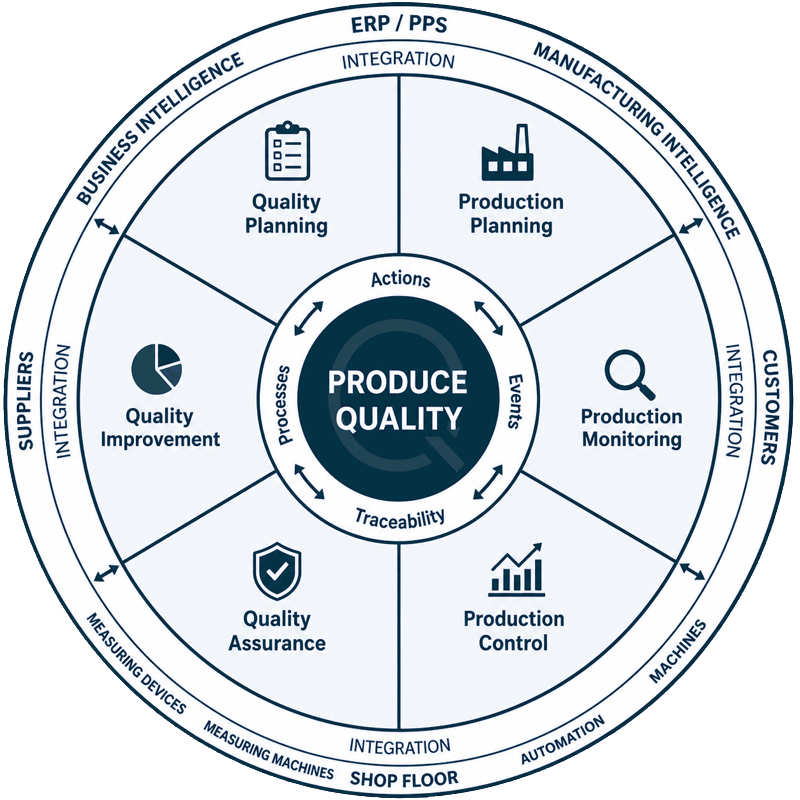
CAQ that produces quality
From inspection planning to operator guidance – modular, integrable, and SAP-compatible
- Significantly reduced inspection effort through CTQ and adaptive inspection strategies
- Zero-defect approach through inline inspection and machine integration
- End-to-end SAP integration and shopfloor connectivity
More than 45 years in manufacturing