What Is an FMEA (Failure Mode and Effects Analysis) in Manufacturing?
A Failure Mode and Effects Analysis (FMEA) is a structured, preventive method for systematically identifying potential failures and for analyzing and prioritizing their causes and effects before those failures actually occur. It is based on the harmonized AIAG-VDA FMEA Handbook, which unifies the previously separate AIAG and VDA methodologies. An FMEA provides a structured risk assessment; it is not an inspection method and replaces neither inspection plans nor operational process controls.
How Is FMEA Positioned Within Quality Management?
Within quality management, FMEA is anchored as a preventive element of quality assurance. Within a quality management system based on ISO 9001, it supports in particular the risk-based thinking required by the standard and the systematic planning of processes and actions, without ISO 9001 prescribing FMEA as a specific method.
What Is the Underlying Logic of FMEA?
The methodological logic of FMEA is based on three assessment dimensions that are rated for each potential failure mode:
- Severity: the seriousness of a failure’s effect on the downstream process, the product, or the customer.
- Occurrence: the likelihood that the underlying failure cause will occur.
- Detection: the likelihood that an existing detection control will identify the failure or its cause before it has an effect.
These three dimensions allow different potential failure modes to be classified on a comparable basis, without in themselves prescribing specific actions. The AIAG-VDA FMEA Handbook distinguishes two types of controls with different effects on the rating: prevention controls act on the failure cause itself and therefore lower the Occurrence rating, while detection controls increase the likelihood of identifying a failure or its cause that has already occurred before it takes effect, and therefore influence the Detection rating. Both types of controls are documented separately in the risk analysis.
How Are Risks Rated in FMEA – RPN or Action Priority?
Traditionally, the three rating dimensions were combined into the Risk Priority Number (RPN), calculated as Severity × Occurrence × Detection. The harmonized AIAG-VDA FMEA Handbook (2019) replaced this practice with Action Priority (AP). Instead of a calculated figure, AP assigns each potential failure mode to the categories High, Medium, or Low using a defined lookup table in which Severity is given priority. The reason for this change was a well-known weakness of the RPN: a safety-relevant failure with a low likelihood of occurrence could produce the same numerical value as a frequent but non-critical failure, and both were therefore prioritized equally by calculation. With Action Priority, high Severity can no longer be offset by a favorable Occurrence or a good Detection rating. Organizations that continue to track RPN values for internal trend analysis use them, according to the AIAG-VDA Handbook, as a supplementary metric, not as the sole basis for decisions.
What Is the Methodological Structure of FMEA?
The AIAG-VDA FMEA Handbook describes a seven-step approach that replaces the previously separate approaches of AIAG (4th edition) and VDA Volume 4 and has since formed the shared methodological basis for FMEA practitioners in both systems:
- Planning and preparation. The project scope, analysis boundaries, and FMEA team are defined; if a comparable analysis already exists, it serves as a foundation FMEA for further work.
- Structure analysis. The system, product, or process under consideration is broken down into its elements, usually represented as a structure tree or block diagram. Interfaces and interactions between the elements are captured in the process.
- Function analysis. Each structural element is assigned its requirements or functions. Linking these functions produces a function network that shows the cause-and-effect relationships between the levels.
- Failure analysis. For each function, possible malfunctions are identified along the so-called failure chain: the failure mode sits at the structural level under consideration, the resulting failure effect at the next higher level, and the underlying failure cause at the next lower level. Several linked failure chains form a failure network, which serves as the basis for the risk analysis.
- Risk analysis. Existing or planned prevention and detection controls are assigned to the failure causes, Severity, Occurrence, and Detection are rated, and the Action Priority is determined for each failure chain.
- Optimization. For failure causes with a high Action Priority, additional actions are derived, prioritized, and tracked in order to reduce Severity, lower Occurrence, or improve Detection.
- Results documentation. The analysis, the assumptions made, the derived actions, and their implementation status are compiled as evidence of the risk assessment performed.
According to the AIAG-VDA Handbook, an FMEA is developed by an interdisciplinary FMEA team that, depending on the object of analysis, involves design, manufacturing, quality, and other affected functions. Team sessions are usually moderated by a qualified person (FMEA facilitator) to ensure the method is applied correctly and the discussion is structured.
What Types of FMEA Are Distinguished?
Depending on the object of analysis, different types of FMEA are applied:
- System FMEA: analysis of complex systems and the interactions between their components.
- Design FMEA: examination of potential failures in product or design engineering, before the start of series production.
- Process FMEA: analysis of risks within manufacturing or service processes.
- FMEA-MSR (Monitoring and System Response): a supplementary analysis within the Design FMEA for systems that monitor failures during vehicle or product operation and respond with a defined system response, for example electronic safety or driver assistance systems.
The choice of FMEA type depends on the object under consideration and its point in the product development process; the results of a Design FMEA typically feed into the subsequent Process FMEA as an input. For recurring, largely identical systems, components, or processes, an existing FMEA can also be reused and adapted as a foundation FMEA or family FMEA for comparable new applications, instead of creating every analysis entirely from scratch.
How Does FMEA Differ From a Control Plan and SPC?
FMEA is an analytical method for risk identification and does not itself provide operational process monitoring. A control plan translates the critical characteristics and risks identified in the FMEA into concrete, operational inspection and reaction requirements; characteristics that are highlighted because of their importance for safety, regulatory compliance, or function are often marked as special characteristics and carried over into the control plan with separate requirements. Statistical process control is used for the ongoing monitoring of defined process characteristics based on measured values over time. FMEA, control plan, and statistical process control therefore fulfill distinct roles that build on one another: FMEA identifies and prioritizes risks, the control plan derives operational inspection measures from them, and statistical process control (SPC) monitors actual process performance.
What Role Does FMEA Play in Industrial Manufacturing?
In manufacturing, FMEA is used in particular for the preventive safeguarding of products and series processes before failures occur in series production. In the automotive industry, evidence of a completed Design or Process FMEA is regularly part of the initial sample inspection within the PPAP process. If the design, the process, or the production equipment used changes, or if new failure causes become known, the corresponding FMEA is revised rather than started from scratch.
FAQ – Frequently Asked Questions About FMEA
What is the goal of an FMEA?
The goal of an FMEA is the early, structured identification of potential failures and the comparable assessment and prioritization of the associated risks before those failures occur.
Is FMEA a mandatory requirement?
No. FMEA is not mandated by standards as such, but in the automotive sector it is regularly required as a recognized method for risk analysis via IATF 16949 and customer-specific requirements.
Why has the Risk Priority Number (RPN) been replaced by Action Priority (AP)?
Since the harmonized AIAG-VDA FMEA Handbook of 2019, the Risk Priority Number has been replaced by Action Priority, which assigns each potential failure mode to High, Medium, or Low using a defined table and gives priority weighting to Severity.
Does an FMEA replace inspections or controls?
No. FMEA is a preventive analytical method and does not replace operational inspection or monitoring measures such as a control plan or statistical process control.
What distinguishes System, Design, and Process FMEA?
System FMEA examines interactions within complex systems, Design FMEA examines potential failures in product or design engineering, and Process FMEA examines risks within manufacturing or service processes.
What is an FMEA-MSR?
FMEA-MSR (Monitoring and System Response) is a supplementary analysis within the Design FMEA for systems that monitor failures during operation and respond to them with a defined system response, for example safety-relevant electronic systems.
How many steps does FMEA comprise under the AIAG-VDA Handbook?
The harmonized AIAG-VDA FMEA Handbook describes a seven-step approach, from planning through structure, function, failure, and risk analysis to optimization and results documentation.
Is FMEA dependent on software?
The method is fundamentally independent of software; IT systems support documentation, rating logic, and evaluation, but do not replace the technical analysis itself.
Standards and Norms
The harmonized AIAG-VDA FMEA Handbook (1st edition, 2019) describes the seven-step methodology, the rating tables for Severity, Occurrence, and Detection, and the Action Priority logic for risk assessment, and is one of the central reference sources for FMEA in the automotive sector. ISO 31000 provides general principles and guidelines for risk management, to which the risk-based logic of FMEA is methodologically related, without ISO 31000 prescribing FMEA as a specific procedure. ISO Guide 73 defines the underlying risk management terminology. Within a quality management system based on ISO 9001, FMEA supports the risk-based thinking required by the standard. In the automotive sector, IATF 16949 additionally requires the application of suitable methods for risk analysis.
Further reading: Quality management, Quality assurance, Statistical process control, ISO 9001, Risk management, Fault tree analysis (Wikipedia).
Further Internal Content
- Control plan as the operational implementation of identified risks
- Action management for tracking derived actions
- FMEA software in the CAQ system
AI-assisted · Editing and publication: Christian Sedlag · Last updated: 28 October 2026
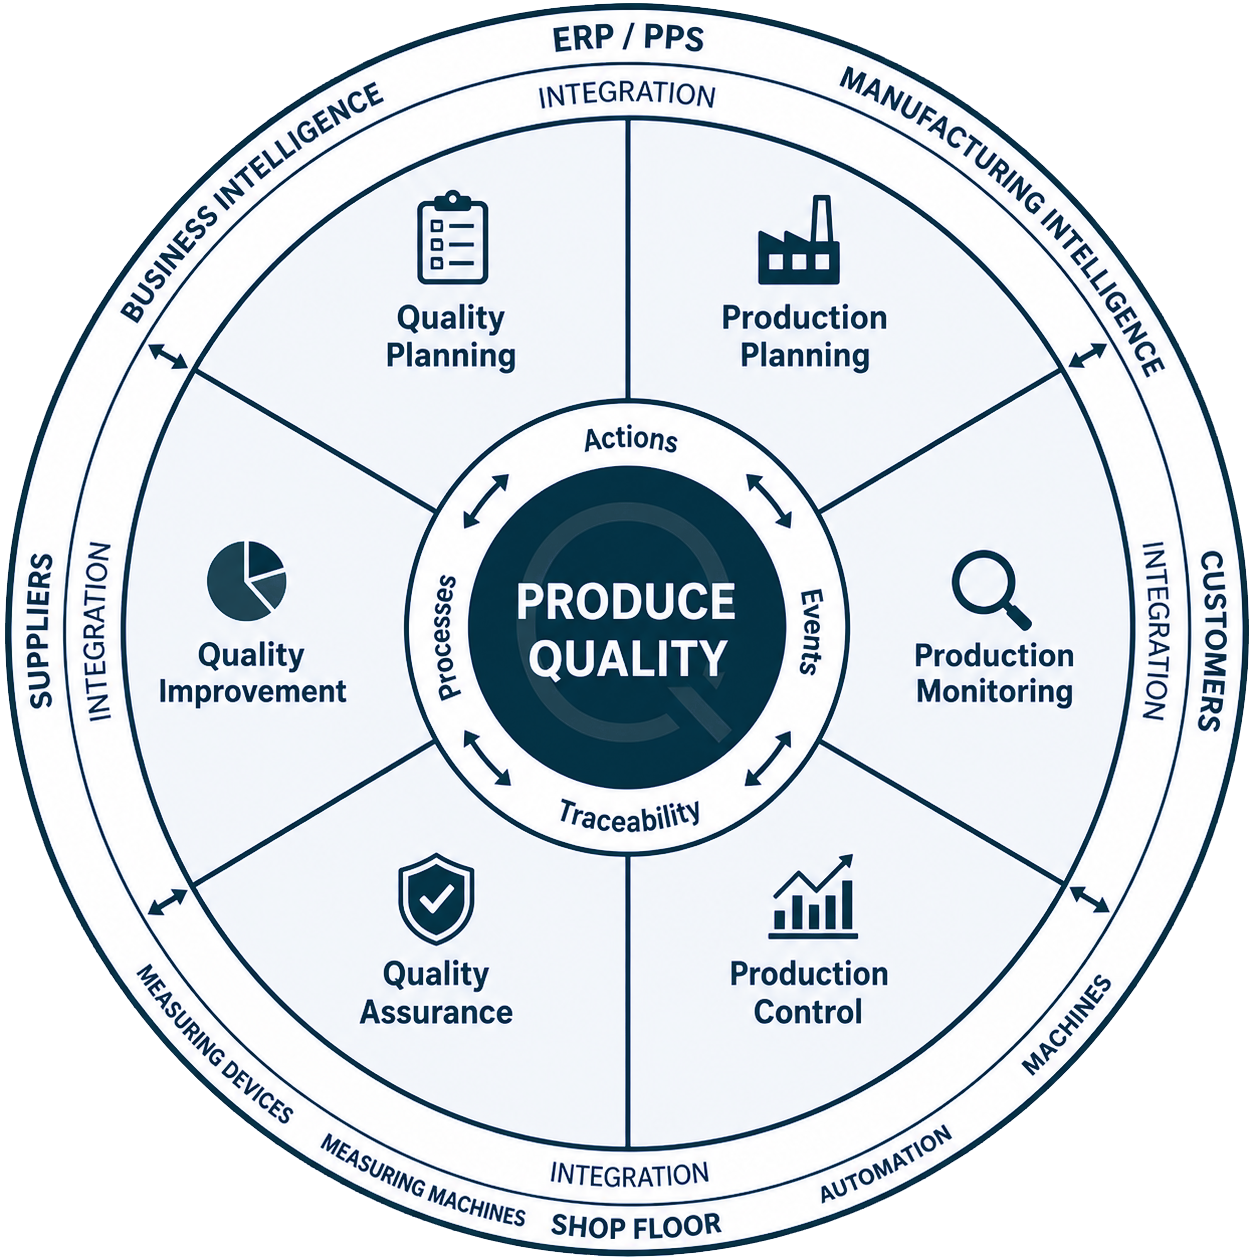
CAQ that produces quality
From inspection planning to operator guidance – modular, integrable, and SAP-compatible
- Significantly reduced inspection effort through CTQ and adaptive inspection strategies
- Zero-defect approach through inline inspection and machine integration
- End-to-end SAP integration and shopfloor connectivity
More than 45 years in manufacturing